Biting into your favorite artisanal snack or pouring a signature gourmet beverage delivers a familiar experience every single time. Most consumers take this batch-to-batch perfection for granted, rarely considering the complex logistical dance happening behind factory doors.
Behind every household food brand lies a sophisticated supply chain network engineered to protect product integrity over time. Maintaining identical flavor profiles, texture, and shelf life across millions of retail units requires absolute operational precision.
Steer clear of assuming that premium food quality depends solely on high-grade raw ingredients and secret recipes. Leading high-end food manufacturers rely just as heavily on robust machinery maintenance, strict temperature controls, and seamless component sourcing.
Start examining how industrial food processing facilities prevent minor mechanical breakdowns from spiraling into costly retail shelf shortages. Unsung supply chain systems keep your favorite grocery products fresh, safe, and readily available every single day.
Managing Factory Procurement and Equipment Maintenance
Streamlining Plant Operations and Vendor Relationships
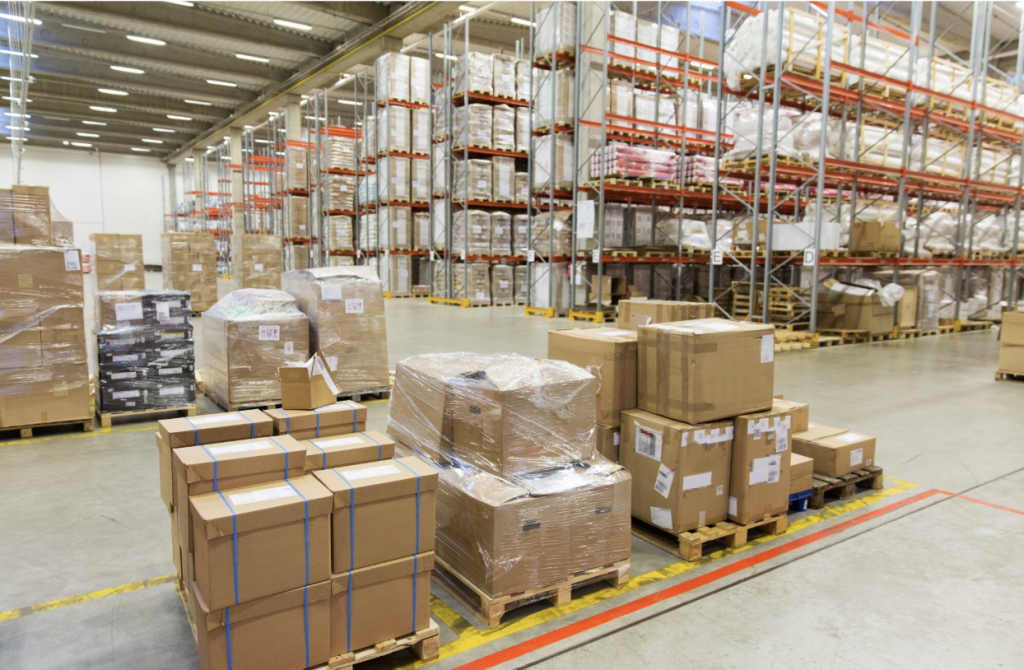
Keeping a food processing plant running smoothly requires constant access to specialized industrial hardware, spare parts, and sanitation supplies. Facility managers balance hundreds of moving parts, from conveyor belts and food-grade lubricants to automated packaging sensors.
Partnering with dedicated procurement partners like All Star Purchasing mro suppliers enables growing food brands to streamline vendor management, leverage collective buying power, and secure critical replacement parts before equipment failures impact production schedules.
Centralizing your purchasing workflow eliminates administrative confusion across regional manufacturing facilities.
Compliance standards published by the U.S. Food and Drug Administration emphasize that proactive equipment servicing and verified vendor audits are essential for maintaining food safety and preventing line contamination. Neglecting routine calibration leads to dangerous processing variances and costly product recalls.
Selecting reliable industrial MRO suppliers protects your manufacturing line from unexpected mechanical halts during peak market demand cycles. Structured facility maintenance protocols preserve the exact taste, aroma, and texture loyal consumers expect.
Building Operational Resilience Against Production Downtime
Essential Strategies for Food Manufacturing Consistency
Preventing unexpected factory delays requires a proactive approach to overall facility maintenance and supply chain logistics. Before scaling your production volume, implement these essential core operational safeguards across all your processing plants:
- Establish standardized preventative maintenance schedules for all processing machinery
- Consolidate maintenance and repair purchasing under unified vendor agreements
- Maintain safety stock for high-wear mechanical parts vulnerable to sudden breakdown
Integrating smart inventory tracking systems prevents expensive emergency shipping fees when critical mechanical components wear out unexpectedly. Establishing strong operational foundations keeps high-speed processing lines moving smoothly without interruption.
Eliminating Inventory Bottlenecks Across Processing Facilities
Supply chain research from McKinsey & Company highlights that enterprise MRO optimization eliminates maverick spending while cutting facility maintenance overhead by as much as twenty percent. Reducing redundant inventory holdings frees up vital working capital for brand expansion and product development.
Monitoring spare parts consumption helps experienced plant directors spot recurring machinery issues before major breakdowns occur across the facility. Data-driven maintenance tracking turns chaotic factory repairs into predictable monthly operational expenses.
Eliminate rogue purchasing habits across individual plants to maintain strict quality standards across all production sites nationwide. Unified operational control preserves your brand reputation as your commercial manufacturing footprint grows.
The Behind-the-Scenes Supply Chain That Keeps Premium Food Brands Consistent
Understanding the behind-the-scenes supply chain that keeps premium food brands consistent helps consumers appreciate the complex engineering behind daily groceries. Seamless maintenance, reliable procurement, and strict quality safeguards ensure your favorite snacks taste perfect every time.
Audit your processing facility operations today to identify vulnerable supply bottlenecks before they disrupt your retail distribution network nationwide. Invest in trusted procurement partnerships to build a resilient, future-proof manufacturing operation for years to come.
Author
Written by
Recent Posts
Sectional Sofa vs. Regular Sofa: Which One is Best for You?
Sober and Injured: How to Manage Pain Treatment After a Massachusetts Slip and Fall
Flexible Liquidity Options Are Reshaping How Modern Professionals Handle Unexpected Expenses
5 Best At-Home Teeth Whitening Kits for a Brighter Smile in 2026
From Spa Retreats to Aesthetic Care, the Luxury Travel Itinerary Is Changing
Categories
- Art
- Articles
- Business of Luxury
- Celebrities
- Culture
- Entertainment
- Events
- Faces of Summer 2026
- Fashion
- Fashion & Style
- Featured
- Finance
- Food, Spirits, Wine
- Hamptons
- Hamptons Celebrities
- Health
- Health & Beauty
- Lifestyle
- Luxury Lifestyle
- Press
- Profiles
- Real Estate
- Technology
- The Chronicles
- Travel
- Uncategorized
- Weddings